
Three processes, each with its own character.
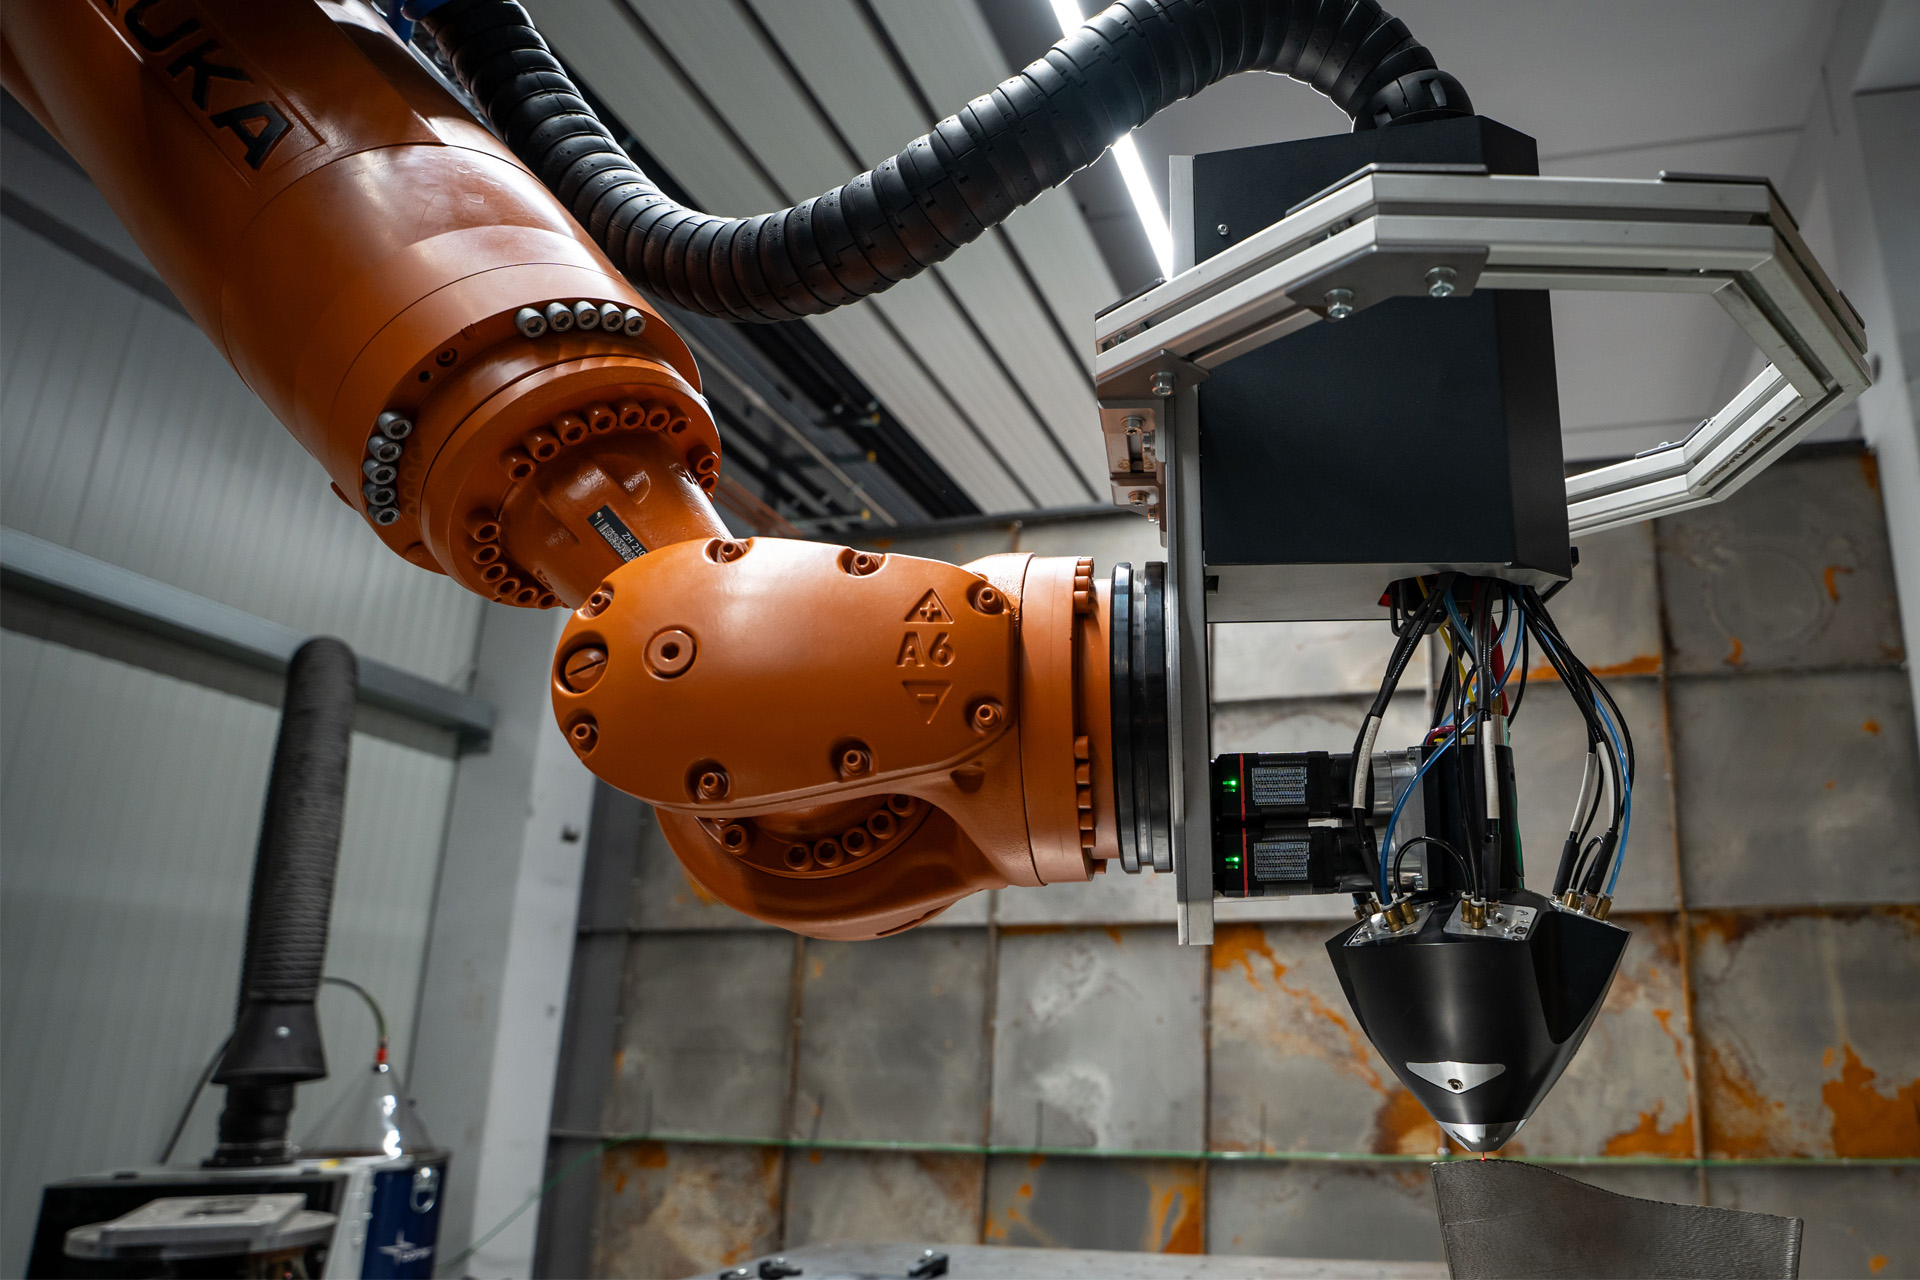
Laser Wire DED, WAAM and SAAM belong to the family of wire-based metal deposition processes. All three build up metal layer by layer from wire. They differ mainly in energy source, protection of the melt pool, deposition rate and geometric resolution.
Laser Wire DED: controlled energy input.
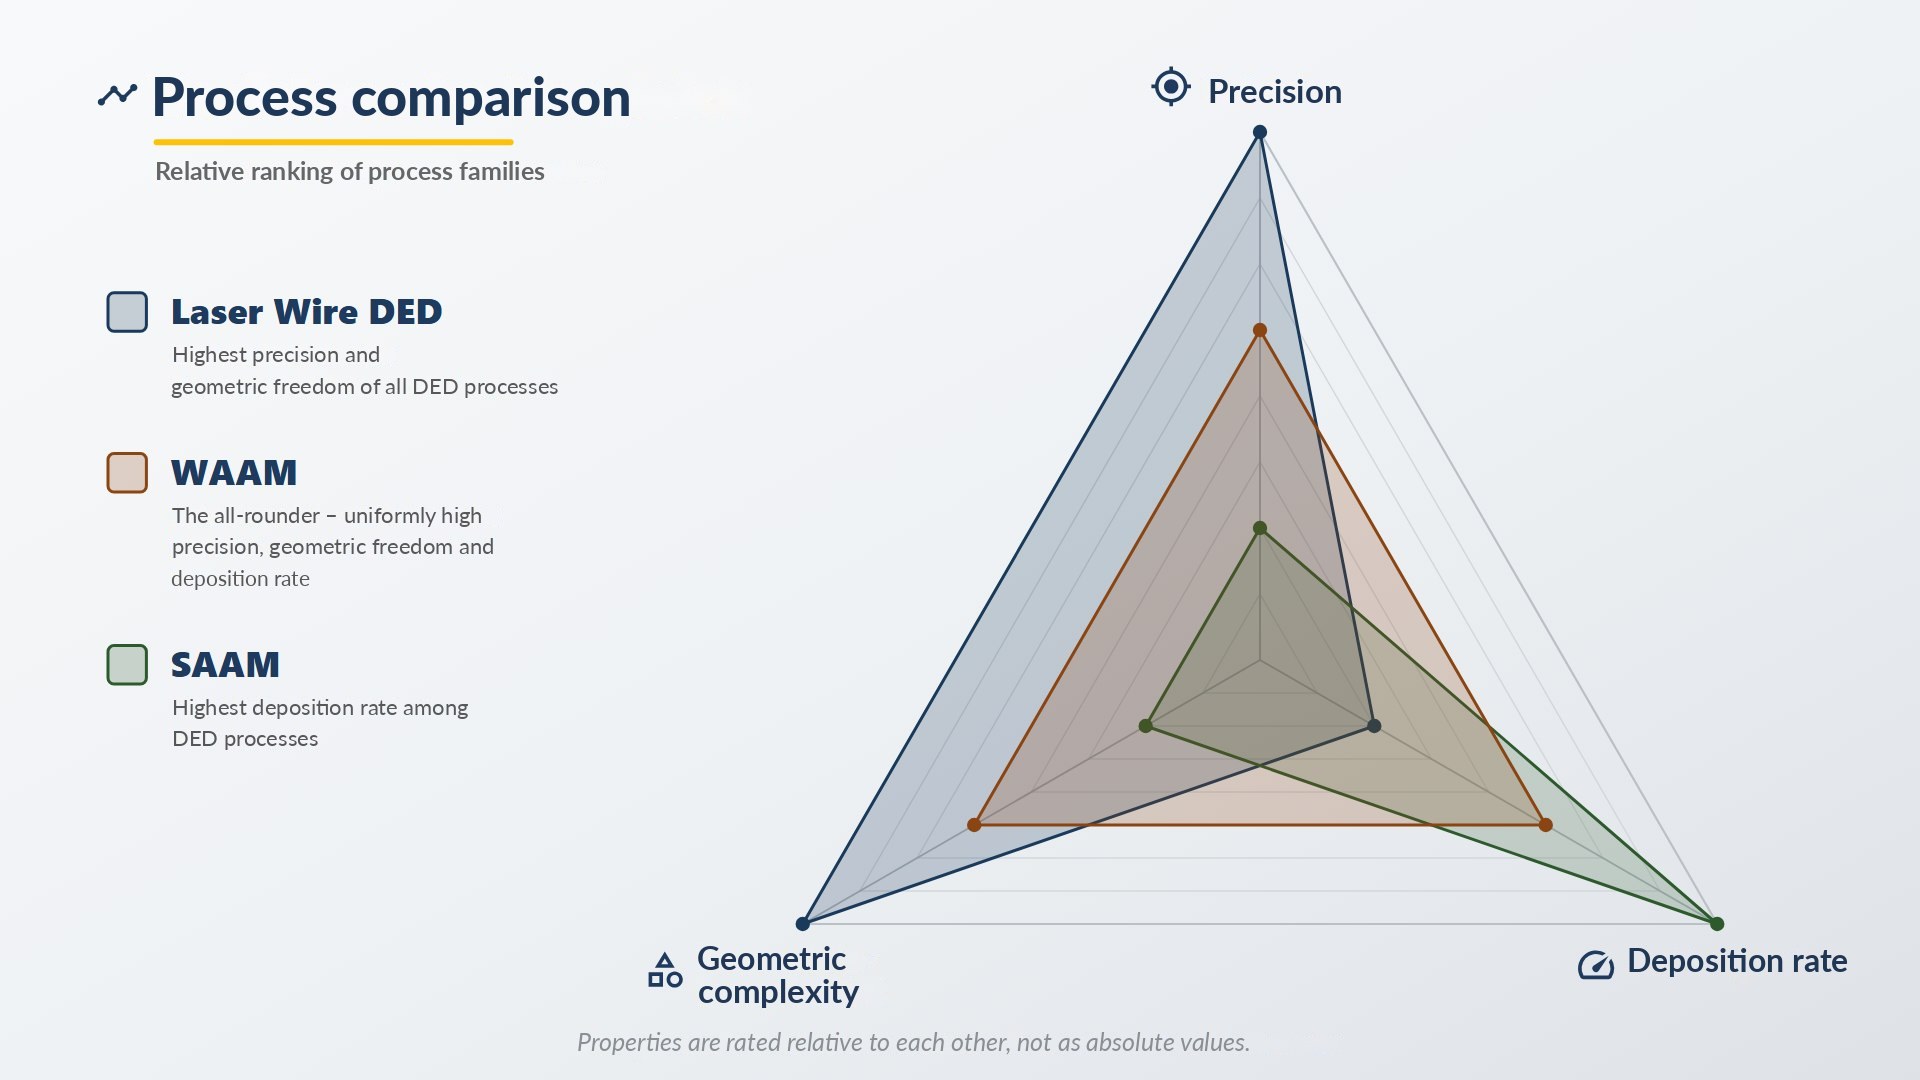
In Laser Wire DED, metal wire is locally melted with a laser and deposited selectively. The process is particularly suitable when controlled heat input, finer structures, and higher geometric quality matter.
- Precise energy input
- Controlled melt pool
- Finer weld beads
- Good basis for hybrid post-processing
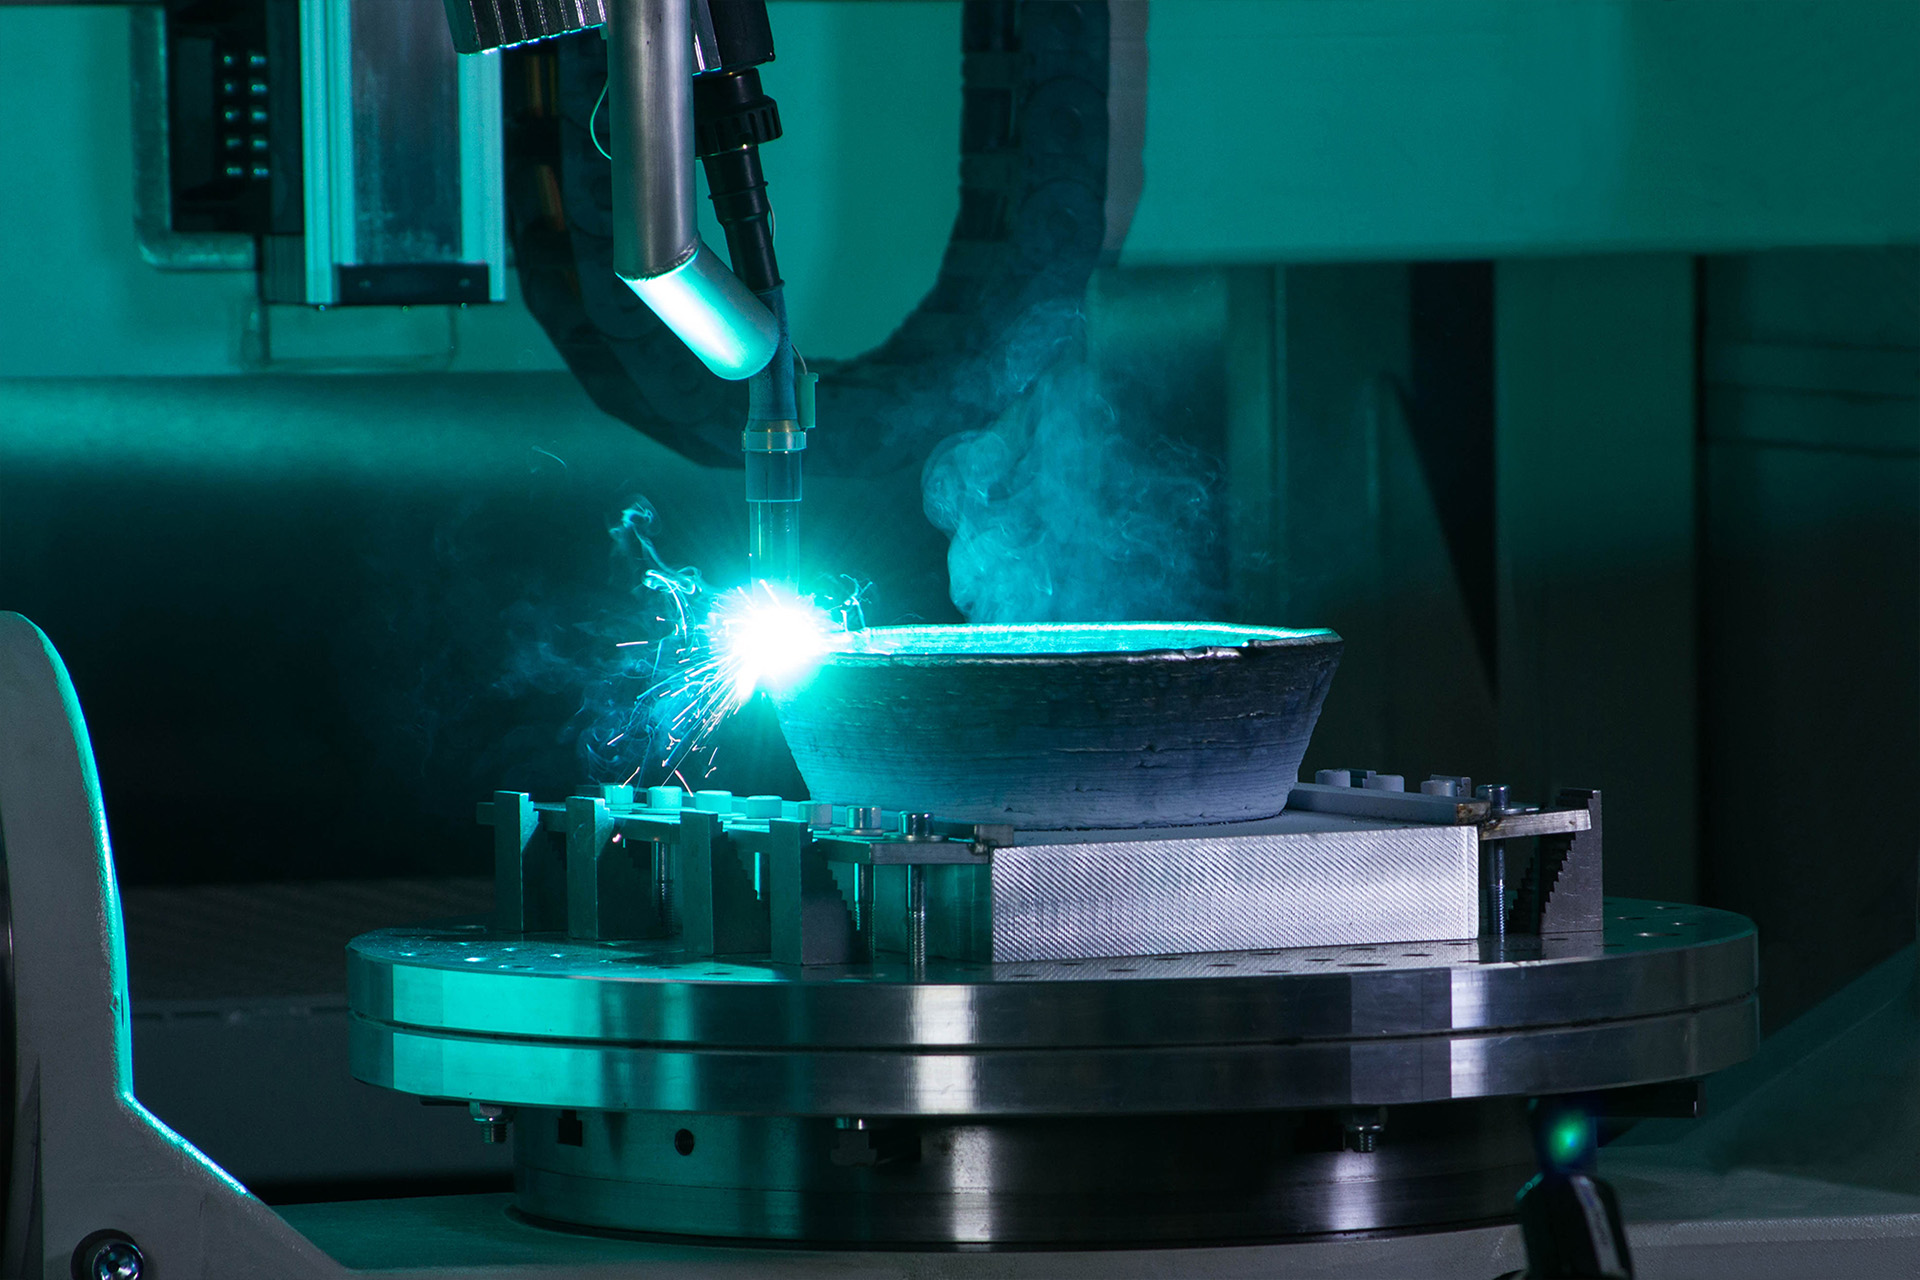
WAAM: massive build-up with an arc.
WAAM uses an arc as the energy source and processes metal wire at a high deposition rate. The process becomes particularly interesting when large volumes are to be built up economically.
- High deposition rate
- Large parts
- Robust process basis
- Economical with a lot of material volume
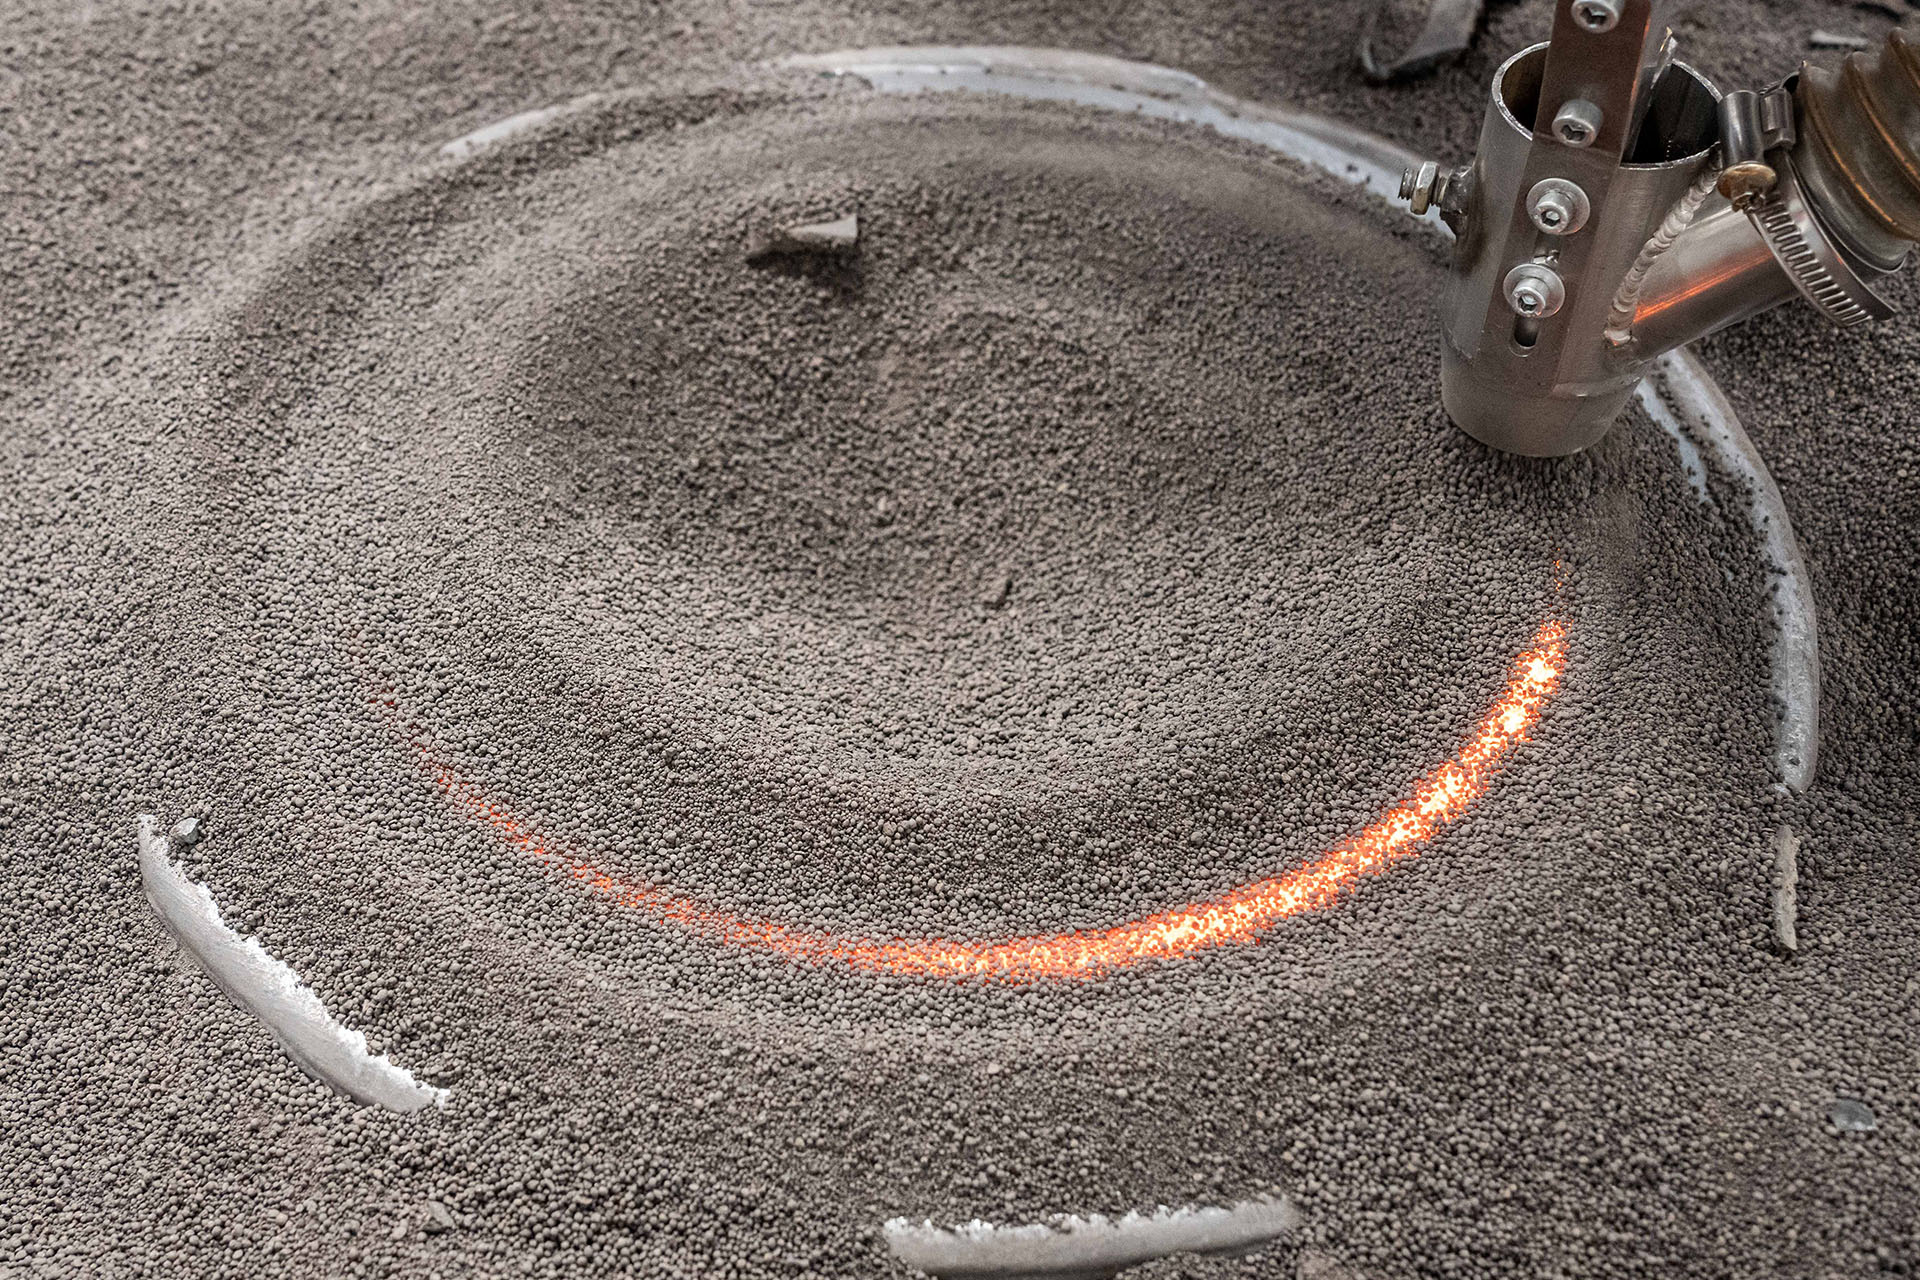
SAAM: high deposition through submerged arc welding.
SAAM uses submerged arc welding for layer-by-layer metal build-up. An arc melts the fed wire under a protective layer of flux. The slag that forms is removed before the build continues. The process is particularly suited to large metal blanks with a high build volume and subsequent machining.
- Submerged arc process
- High deposition rate
- Large metal blanks
- Subsequent machining of functional surfaces
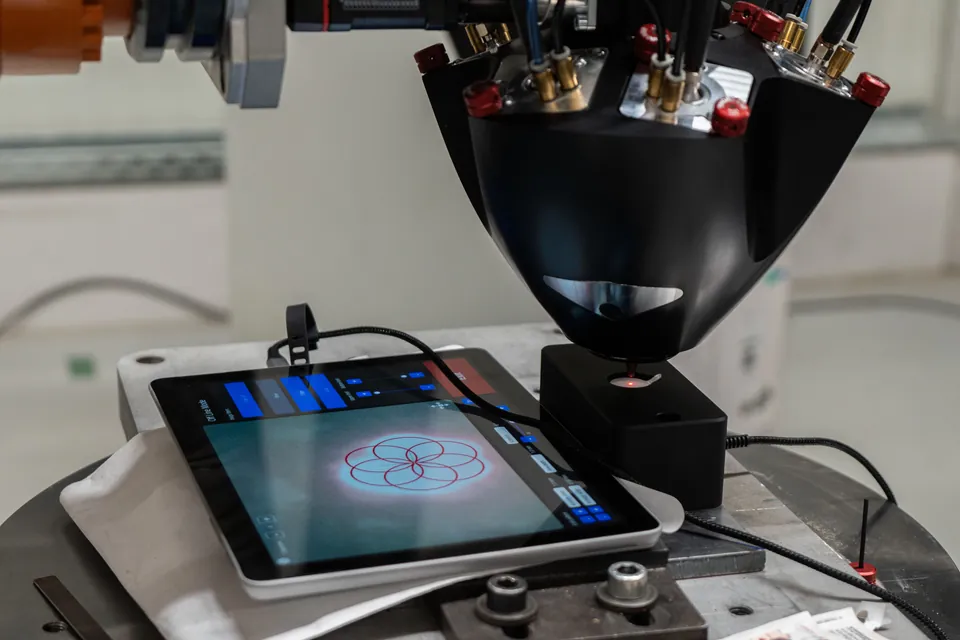
At FIT
The systems behind the three processes
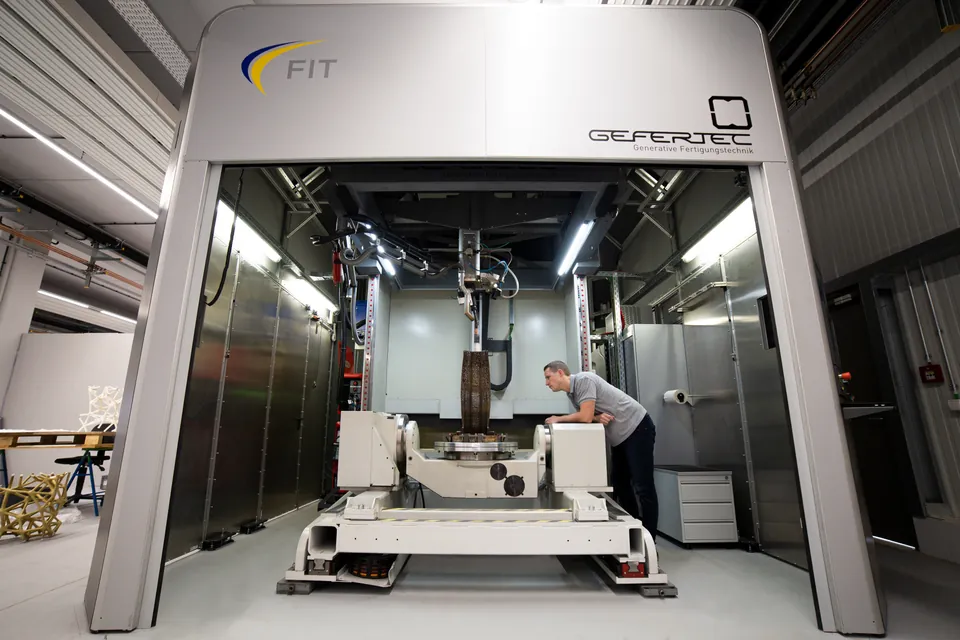
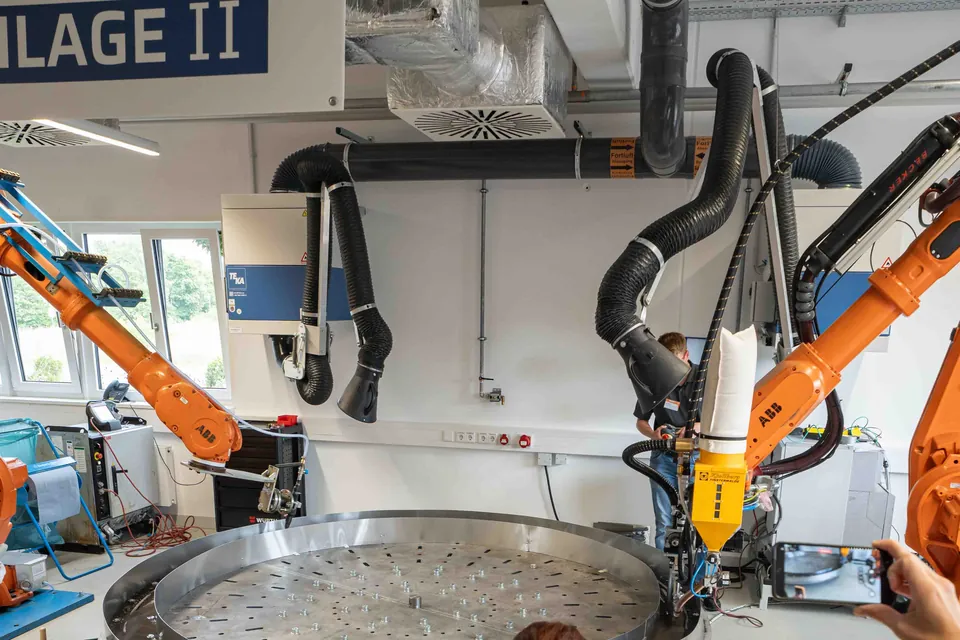
The images above are schematic illustrations. The photos show the systems themselves: the laser wire head, the WAAM system in FIT production, and the SAAM system at the Technologie-Campus.
Not better or worse. Different.
The right choice depends not only on the material. Decisive are part size, geometry, heat input, accessibility, target accuracy, and post-processing.
Laser Wire DED
precise, fine, highest geometric freedom
WAAM
balanced, versatile, the all-rounder
SAAM
large, fast, highest deposition rate
The process is only the beginning.
Whether a part is truly suitable is decided by geometry: overhangs, heat nodes, accessibility, build direction, and post-processing determine the real effort.